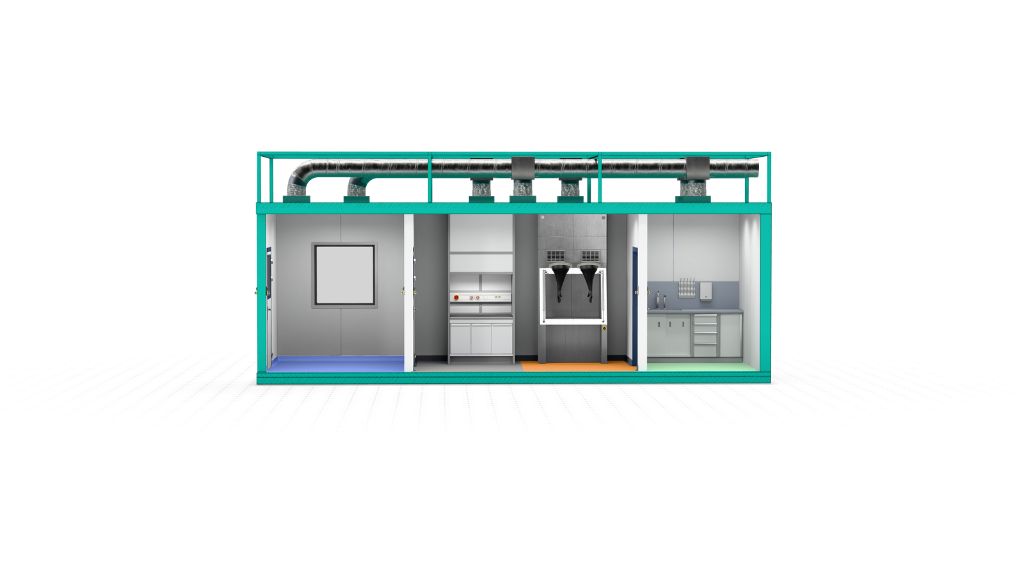
Cleanrooms
Certified floor coatings and specialist sealants provide complete cleanroom solutions for modular construction. Designed for demanding hygienic environments, the systems offer durability, compliance, and performance-enhancing features including abrasion resistance, electrical conductivity, and antimicrobial protection.
Modular construction is increasingly used for cleanrooms and controlled environments in healthcare, laboratories and industry.
Cleanrooms demand low-emission solutions and systems that support strict hygiene standards, long-term durability, and regulatory compliance. Integrated flooring, sealing, and bonding solutions help create robust environments that can withstand intensive cleaning regimes while maintaining performance over time.
High-performance flooring systems provide seamless, easy-to-clean surfaces with options for enhanced abrasion resistance, electrical conductivity, and antimicrobial protection. Complementary sealants and adhesives support the secure bonding of components and help ensure hygienic, low-emission finishes throughout the facility.
Airtightness is another critical consideration in cleanroom design, helping to control contamination, maintain pressure differentials, and improve energy efficiency. Specialist sealing solutions can contribute to a continuous building envelope, reducing air leakage at interfaces and junctions.
Where required, passive fire protection systems can also be incorporated to help maintain compartmentation and support fire safety objectives without compromising cleanroom performance. Together, these solutions provide a coordinated approach to delivering compliant, high-performing modular cleanroom environments.